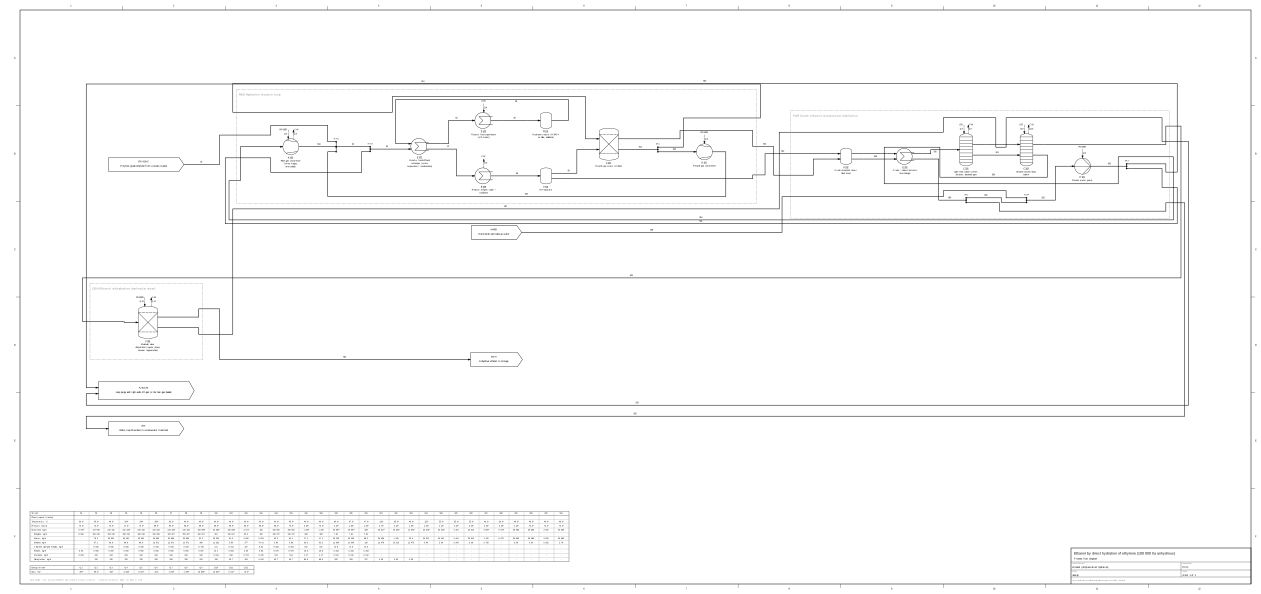
Ethylene from a steam cracker outside the boundary joins the recycle gas, takes up process water (0.35 mol per mol ethylene) and is heated against the reactor effluent and with HP steam to 240 C. About 5 % of the ethylene is hydrated per pass in an adiabatic bed at about 7 MPa (patent literature: US 4003952, US 5349096). The effluent is cooled, the crude ethanol separated and the gas scrubbed with water and recycled; a small purge controls the inerts. The crude (about 12 mol% ethanol) is flashed, freed of ether and butenes in a light-ends column, concentrated to 93 wt% and dehydrated on molecular sieves. Fermentation, the dominant route for ethanol by volume, is not designed here.
All values are concept estimates: the reactor outlet is calculated by cheme from a sourced conversion with assumed selectivities, the separators are specified splits and the duties come from an independent script (see DESIGN.md of the engineering files).