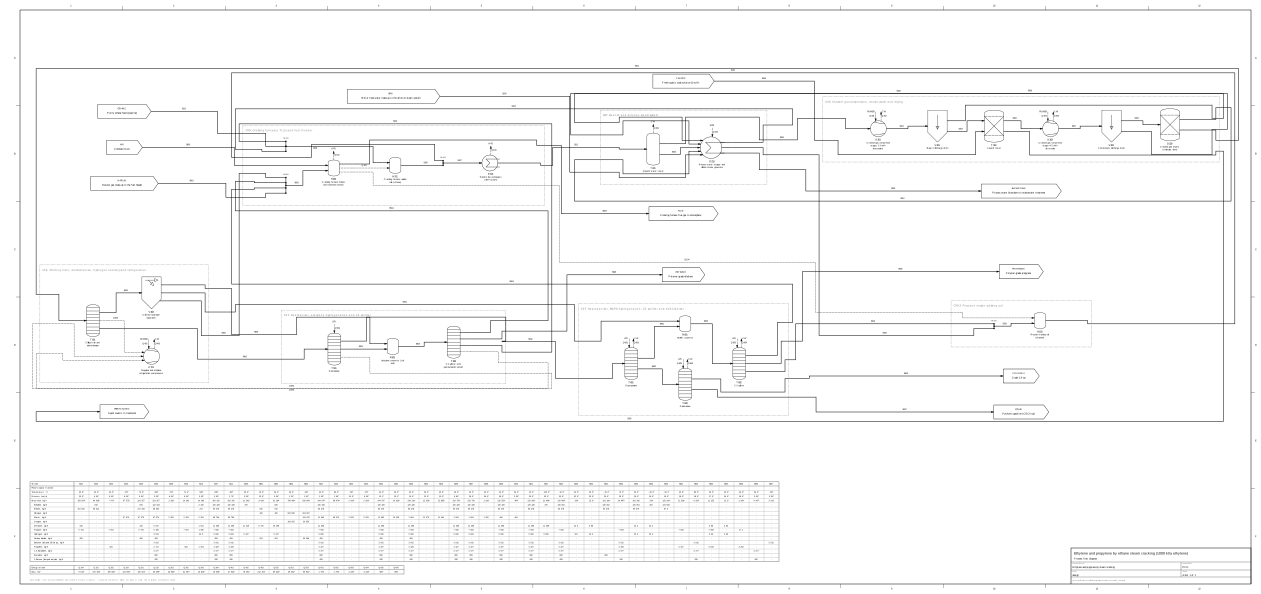
Purity ethane and the recycled ethane are cracked with dilution steam at a coil outlet of 840 C; the recycled propane has its own coil. The furnace is a conversion model that reproduces the once-through ethane and propane yields of the EU BREF on large volume organic chemicals (2017, Table 3.3): a sourced yield model, not kinetics. The cracked gas raises SHP steam in the transfer line exchangers, is quenched with water (the condensate becomes dilution steam again), compressed in five stages with a caustic wash, dried and separated at low temperature: demethaniser (tail gas and hydrogen to the furnace fuel), deethaniser, acetylene converter, C2 splitter, depropaniser, MAPD converter, C3 splitter and debutaniser. The tail gas and a natural-gas make-up fire the furnaces.
The separations are specified splits from an independent balance script, and the energy figures rest on ideal-gas enthalpies: core has no qualified property package for C2+ hydrocarbon mixtures yet. See DESIGN.md for every assumption and gated step.