Natural gas processing (amine CO2 removal, TEG dehydration, turbo-expander NGL recovery)
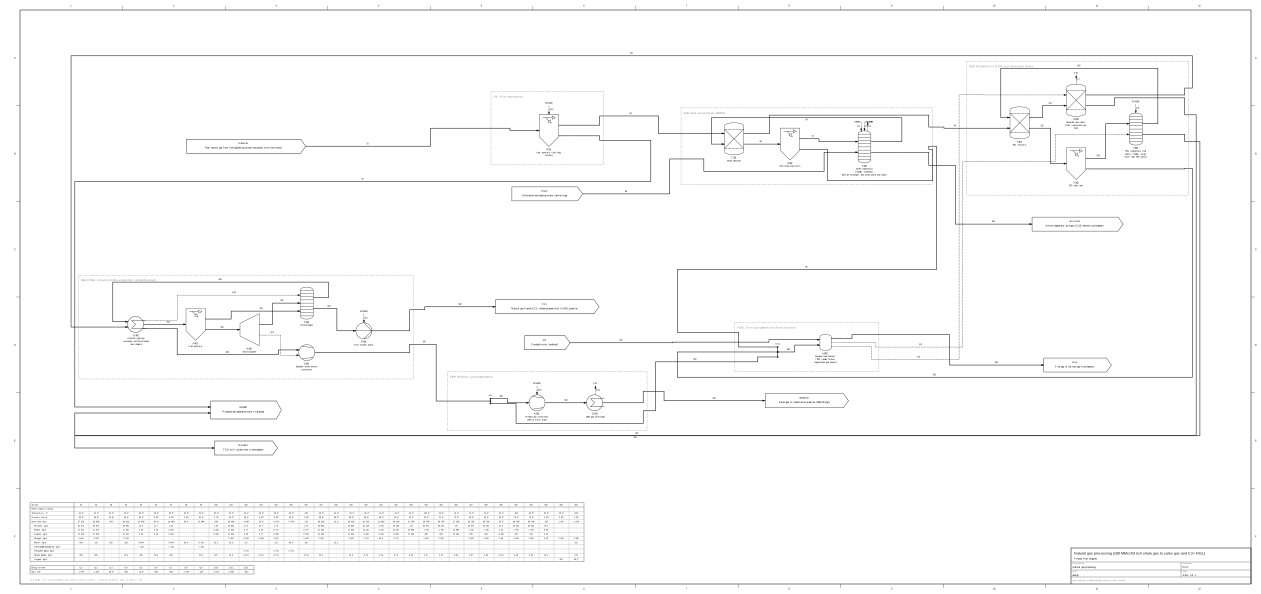
A sweet, CO2-bearing rich shale gas (100 MMscf/d) treated to pipeline sales gas and a C2+ NGL: inlet separation, MDEA CO2 removal, TEG and molecular sieve dehydration, turbo-expander NGL recovery and electric residue compression. Concept stage, sourced feed, assumed basis.
Research outputNot engineering advice and not an approved design: do not use it for construction, operation or safety decisions. What this means
Overview
Raw gas from a shale gathering system (Barnett well 2 composition of Bullin and Krouskop
2009: 81.2 % CH4, 11.8 % C2H6, 5.2 % C3H8, 0.3 % CO2, 1.5 % N2, no H2S) enters at 6000 kPa(a)
and 40 degC. Free water is separated; an MDEA unit removes the CO2 to 50 ppmv so that it
cannot freeze in the cold section and vents the acid gas; a TEG unit dries the gas to the
pipeline water specification and molecular sieve beds polish it for the cryogenic section.
A gas-subcooled-process type turbo-expander plant recovers 90 % of the ethane and 98 % of
the propane as a C2+ NGL; the residue gas is recompressed by the expander-driven booster and
an electric-motor compressor to 7000 kPa(a). Flash gases and a small residue-gas draw fire
the TEG reboiler and the regeneration gas heater. No sulfur recovery: the sourced feed has
no H2S.
All values are concept estimates from a specified-split balance (recoveries and removal
depths from open sources or ASSUMED); no property package of ChemE-as-Code is yet
benchmarked for C2/C3-rich natural gas, aqueous MDEA or TEG, so phase behaviour, the cold-box
energy balance and compressor duties are ideal-gas estimates. See DESIGN.md.
Capacity
100 MMscf/d raw gas (dry basis, 60 degF, 14.696 psia) = 96.7 t/h; 68.7 t/h sales gas (83.7 MMscf/d) and 27.3 t/h C2+ NGL (ASSUMED capacity)
Operation
8,000 h/a
Location
generic US onshore shale gas area (Barnett-type), not chosen
Engineering gates
Concept and feasibility (no results yet)
Maintainers
Artur Schweidtmann
Design basis and assumptions (4)
D-001 boundary: raw gas at the plant inlet to sales gas and C2+ NGL at their pipelines; no field compression, no NGL fractionation, no utility generation, no storage
D-002 no sulfur recovery: the sourced feed reports no H2S
D-006 the balance is a specified-split model (scripts/balance.py); no qualified property package (D-012)
Construction, transport and end of life are outside the preliminary LCI (D-014)
The interactive model (drawings, streams, 3D) is made for larger screens.
Snapshot of c3ab348, cheme-as-code 1.6.0.
What goes in and out
In
Raw natural gasFeedstockfeed:RAWGAS: raw natural gas from field gathering, water-saturated, 1.42 kg/kg sales gas (unallocated)
WaterFeedstockDemineralised make-up water of the amine loop (feed:DMW), 0.64 g per kg sales gas (allocated)
Out
MethaneMain productproduct:SALESGAS, sales gas to the transmission pipeline (7000 kPa(a)), taken as methane like the library's natural-gas consumers; no inventory_key, since the study's energy property is not pure methane's
Natural gas liquidsCo-productC2+ natural gas liquids (ethane-propane mix) to the NGL pipeline
Carbon dioxideEmissionReservoir CO2 vented with the amine acid gas (627 kg/h) and combustion CO2 of the fired heaters (278 kg/h); 9.5 g per kg sales gas (allocated)
MethaneEmissionMethane slip of the amine regenerator and TEG still and unburnt methane of the heaters, 3.05 kg/h; fugitive and non-routine methane not yet estimated
Utilities:Electricity (3.99 MW, of which the residue compressor K-501 3.67 MW (ideal-gas estimate); a possible propane chiller (up to about 1.5 MW, D-016) is not included), Steam (LP steam 450 kPa(a), 1.08 MW, amine reboiler (ASSUMED steam ratio)), Cooling water (30/40 C (ASSUMED), 6.85 MW)
Each reaction's page has the conversion, heat of reaction, catalyst and sources this process states, next to those of other processes with the same reaction. All reactions
Life cycle assessment
0.0105kg CO2-eqPreliminarypartial, 14 data gaps
Climate change per 1 kg Sales gas, gate-to-gate
Main contributors
CO2 to the environment90.8 %
CH4 to the environment9.1 %
N2O to the environment (estimated)0.13 %
Contributions, baseline
Each flow of the inventory into its phase, the phases into the functional unit; band widths are impacts. Hatched: a credit.
Method and data
Goal
Preliminary gate-to-gate life cycle inventory of natural gas processing for the concept stage: the foreground exchanges of the balanced flowsheet (D-006) per kg of sales gas, with the C2+ NGL as co-product, ready to be linked to background datasets (raw gas production, grid electricity, site steam, cooling water). No impact assessment is claimed.
Functional unit
1 kg Sales gas (1 kg SALESGAS)
Boundary
gate-to-gate
Allocation
energy
Characterisation
Factors kept with the process · GWP100
Data quality
Published factors
Result
partial screening carbon footprint · 14 data gaps
Scenario
Climate change (kg CO2-eq)
baseline
0.01048
Inventory per 1 kg Sales gas (30 flows)
Flow
Phase
Direction
Quantity
Unit
Provenance
Raw natural gas from field gathering (water-saturated, with free water)
operation
input
1.025
kg
given
Demineralised make-up water (amine loop)
operation
input
0.0006394
kg
given
Combustion air (ambient)
operation
input
0.01908
kg
given
LP steam 450 kPa(a) from the site steam system (amine reboiler)
operation
input
0.01133
kWh
assumed
Electric power (AC, grid)
operation
input
0.04188
kWh
assumed
Sales gas to transmission pipeline (7000 kPa(a))
operation
output
1
kg
assumed
Natural gas liquids (C2+, ethane-propane mix) to NGL pipeline
operation
output
0.3967
kg
assumed
Amine regenerator acid gas (CO2) vented to atmosphere
operation
output
0.006822
kg
assumed
TEG still column vent to atmosphere
operation
output
0.001807
kg
assumed
Flue gas of the fuel-gas-fired heaters
operation
output
0.02028
kg
assumed
Produced and separated water to disposal
operation
output
0.007098
kg
assumed
Cooling water return
operation
output
0.07197
kWh
assumed
C2H6 to the environment
operation
output
0.000008721
kg
assumed
C3H8 to the environment
operation
output
0.000005636
kg
assumed
CH4 to the environment
operation
output
0.00003207
kg
assumed
CO2 to the environment
operation
output
0.009511
kg
assumed
H2O to the environment
operation
output
0.004119
kg
assumed
N2 to the environment
operation
output
0.01466
kg
assumed
O2 to the environment
operation
output
0.0005796
kg
assumed
NOx to the environment (estimated)
operation
output
0.000002266
kg
estimated
CO to the environment (estimated)
operation
output
0.000001904
kg
estimated
N2O to the environment (estimated)
operation
output
0.00000004984
kg
estimated
PM to the environment (estimated)
operation
output
0.0000001722
kg
estimated
NMVOC to the environment (estimated)
operation
output
0.0000001246
kg
estimated
MDEA make-up (losses by vaporisation, entrainment, degradation)
operation
input
0.0000197
kg
assumed
Disposal: MDEA make-up (losses by vaporisation, entrainment, degradation) (amine reclaimer residue and degradation products to hazardous waste incineration)
operation
output
0.0000197
kg
assumed
TEG make-up (vaporisation and carry-over losses)
operation
input
0.00001839
kg
assumed
Disposal: TEG make-up (vaporisation and carry-over losses) (spent glycol and filter residue to incineration)
operation
output
0.00001839
kg
assumed
Molecular sieve adsorbent (zeolite 4A), replaced every 4 years
operation
input
0.00001313
kg
assumed
Disposal: Molecular sieve adsorbent (zeolite 4A), replaced every 4 years (spent zeolite to landfill (non-hazardous for sweet gas))
operation
output
0.00001313
kg
assumed
Computed by ChemE-as-Code from lca/README.md, lca/dataset.yaml, lca/factors.yaml, lca/gaps.csv, lca/inventory.csv, lca/lca.yaml, lca/mappings.yaml, lca/results.csv, lca/results.md.
Download it for Brightway, openLCA and other tools.
In the LCI database: system model, datasets and KPIs against the benchmarks
In the LCI database
Status
Preliminary 7 unmapped exchanges. Some exchanges have no background mapping yet: they are exported unlinked and count no burden, so the inventory is incomplete.
System model
attributional, cut-off (methodology 1.1.0)
Allocation
energy (deviation, from study) · product:NGL 27.8 %, product:SALESGAS 72.2 %
Allocation findings
none
Change report
Not available: this build has no change report against an earlier release.
KPI benchmark positions: not available (no benchmarked KPI for this process's datasets).
Maturity and review
Design maturity Concept (claimed): An idea or first flowsheet; numbers are rough. Concept PFD with closed mass, component and element balances (cheme validate, cheme process streams: every block and step within tolerance; the fired heaters as a reactive step with complete combustion). The streams come from an independent specified-split balance (scripts/balance.py): the feed composition is sourced (Bullin and Krouskop 2009, Table 1), the TEG circulation, gas absorption and flash recovery follow EPA Natural Gas STAR, the ethane/propane recoveries sit inside the range of a GSP patent; removal depths, loadings, efficiencies and the cold separator split are ASSUMED. Energy closure is not evaluable in core: no benchmarked property package covers these mixtures. The preliminary gate-to-gate LCI closes in mass and C/H/N/O (consumables excepted, no composition); every background is a gap; fugitive and non-routine methane is not in the inventory (a screening amount of fugitive methane, 0.1 % of the methane processed, is recorded for the cut-off check and would roughly triple the direct GHG; D-017). The electricity (3.99 MW) is probably under-estimated: an order-of-magnitude cold-box check (D-016) leaves a refrigeration deficit that a propane chiller of up to about 1.5 MW electric (up to +40 %) would cover; no chiller is in the balance. Not reviewed. Main products and feeds are listed under chemistry with their chemicals registry entries (issue #251).
Calculation maturity, from the checked evidenceNot assessed
The process has no maturity report (cheme maturity, checks/maturity.json), so no calculation maturity is established.
No level shownThe design maturity (Concept) is the manifest's claim, not evidence. A level appears here once the process's repository holds a current report from cheme maturity --write.
Artifact completeness
Which deliverables exist. They never raise a calculation maturity level: a drawing from unchecked numbers is still unchecked.
Not reported without a maturity report.
Independent review
Not independently reviewed
No independent engineering review yet. Automated checks passing is not a review.
Set by people only. Reaching a calculation maturity level or passing automated checks is not an independent review or an approval.
Where the evidence comes from
Report
processes/natural-gas-processing-1/checks/maturity.json(not in the library)
Natural Gas. Ullmann's Encyclopedia of Industrial Chemistry, Wiley-VCH (route identity from issue #181; full text not read) · doi:10.1002/14356007.a17_073
For the data, cite the Process Atlas paper; for the platform that builds and checks it, the ChemE-as-Code paper.
Schweidtmann, A. M. & Weber, J. M. (2026, in preparation). Process Atlas: an open, git-native, reproducible library and life cycle inventory of chemical processes (working title).
For this process: "Natural gas processing (amine CO2 removal, TEG dehydration, turbo-expander NGL recovery)", ChemE-as-Code process library, version c3ab348.
BibTeX
@unpublished{schweidtmann_process_atlas,
  author = {Schweidtmann, Artur M. and Weber, Jana M.},
  title = {{Process Atlas: an open, git-native, reproducible library and life cycle inventory of chemical processes (working title)}},
  year = {2026},
  url = {https://atlas.cheme-as-code.org},
  note = {in preparation}
}
Schweidtmann, A. M. (2026, in preparation). ChemE-as-Code: An Open-Source Platform for AI-Accelerated Chemical Process Engineering (working title).
BibTeX
@unpublished{schweidtmann_cheme_as_code,
  author = {Schweidtmann, Artur M.},
  title = {{ChemE-as-Code: An Open-Source Platform for AI-Accelerated Chemical Process Engineering (working title)}},
  year = {2026},
  url = {https://cheme-as-code.org},
  note = {in preparation}
}